What Is the Top Manual Block Machine for Global Buyers?
Choosing the right Manual Block Machine is rarely a simple price comparison. Global buyers must examine production capacity, block dimensions, material waste, maintenance access, and operator safety. A machine that performs well in one climate may struggle in another. Moisture, cement quality, power stability, and local aggregate sizes can change the final result.
Dr. S. K. Duggal, a respected civil engineering author and building-materials specialist, emphasized a practical principle: “The strength of concrete depends on the quality of materials and workmanship.” This idea applies directly to block production. Even a strong Manual Block Machine cannot correct poorly graded sand, inaccurate water ratios, or careless curing. Small details matter. Firm moulds. Clean surfaces. Consistent pressure.
This guide explores what makes a top Manual Block Machine suitable for international buyers. It considers steel construction, mould flexibility, daily output, spare-part availability, and training requirements. Supplier communication also deserves attention. Clear drawings and realistic performance data can prevent expensive misunderstandings.
There is no perfect machine.
Some buyers may overvalue output figures and underestimate human effort. Others may choose the lowest quotation and discover hidden costs later. That is a weakness worth admitting. A reliable decision requires practical testing, written specifications, and reference checks from comparable projects. Buyers should also question impressive claims. A dependable machine should produce uniform blocks repeatedly, not only during a short demonstration. This introduction sets a careful direction for comparing equipment, suppliers, and long-term value across different markets.
Global Manual Block Machine Market: Key Types, Uses, and Buyer Criteria
What Is the Top Manual Block Machine for Global Buyers?
Global Manual Block Machine Market: Key Types, Uses, and Buyer Criteria
The best manual block machine depends on production goals, labor conditions, and local materials.
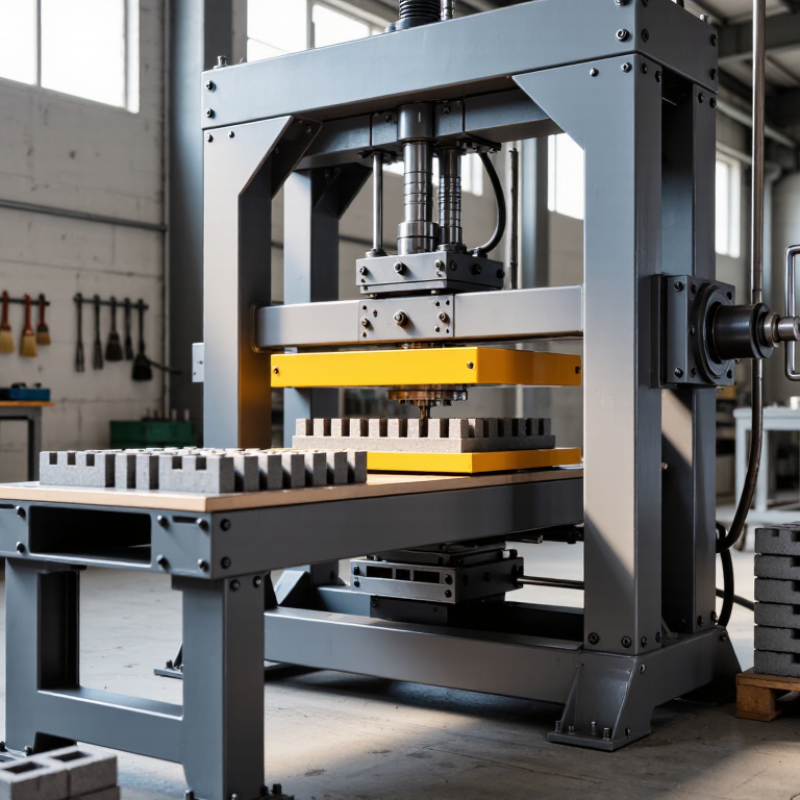
Small contractors often choose lever-operated models for low cost and simple maintenance. Hydraulic manual machines provide more consistent pressure and denser blocks. Vibration-assisted designs can improve compaction, especially for paving units. Each type has limits. A basic lever machine may struggle with high daily output.
These machines commonly produce hollow blocks, solid masonry units, kerbstones, and small paving blocks.
Buyers should examine mold compatibility before comparing prices. A machine with several mold options can support changing construction demand. However, extra molds increase storage and adjustment work. I have found that test production reveals more than attractive specifications. Check block edges, weight variation, demolding speed, and surface cracks using the intended cement and aggregate.
Reliable purchasing requires more than a strong frame. Review steel thickness, weld quality, pressure control, moving-part protection, and replacement-part availability. Ask for operating instructions and realistic capacity figures. Claimed output may assume experienced workers and ideal material moisture. Local electrical needs matter when vibration or hydraulic systems are included. Worker training also affects safety and block consistency. Buyers sometimes overlook after-sales support because the machine appears simple. That choice can become expensive. A short factory inspection or monitored trial may expose weaknesses early, although it cannot predict every site condition.
How ASTM C90 and EN 771-3 Shape Block Quality Requirements
For global buyers, the top manual block machine is not simply the cheapest option. It should help operators produce consistent units under local working conditions. ASTM C90 and EN 771-3 define the quality target, not the machine itself. ASTM C90 focuses on concrete masonry unit strength, dimensions, absorption, density, and durability. EN 771-3 covers aggregate concrete masonry units, declared properties, tolerances, and assessment methods. That distinction matters.
A reliable manual machine should provide repeatable mold filling, controlled compaction, and clean demolding. Adjustable molds can support different block sizes and project requirements. Buyers should measure block length, width, height, weight, and visible defects during trials. Compressive strength tests should follow an approved laboratory method. Moisture content and curing conditions also need records. Some buyers focus only on daily output. That can be a costly mistake. Uneven density may create rejected blocks later. Standards help, but they cannot correct poor aggregates or careless curing.
Tips: Request trial blocks before purchasing. Check dimensions and surface edges carefully. Ask for documented test results and machine setting guidance. Keep ASTM C90 and EN 771-3 requirements in the purchase file. Train operators to inspect every batch. A first trial may reveal weaknesses in the mold, mix, or workflow. That is useful, not embarrassing.
What Is the Top Manual Block Machine for Global Buyers?
How ASTM C90 and EN 771-3 Shape Concrete Masonry Block Quality Requirements
ASTM C90 specifies a minimum average net-area compressive strength of 13.8 MPa for loadbearing concrete masonry units, with no individual unit below 11.7 MPa. EN 771-3 uses declared compressive-strength classes rather than one universal minimum; common classes include 8, 12, 16, and 20 MPa. Buyers should therefore evaluate a manual block machine by its ability to produce consistent density, dimensions, curing quality, and repeatable strength—not only by output capacity.
Comparing Cycle Time, Daily Output, and Mold Capacity Across Machines
What Is the Top Manual Block Machine for Global Buyers?
For global buyers, the best manual block machine is not always the fastest model. Cycle time, daily output, and mold capacity reveal its practical value. A typical manual press may complete one cycle in 30 to 60 seconds. The exact time depends on material moisture, filling speed, compaction, and operator experience. Small differences matter. Ten extra seconds can reduce production across a long workday.
Daily output should be calculated from real working conditions, not the advertised maximum. A machine producing 500 blocks per shift may perform closer to 350 blocks after mold cleaning, mix preparation, pallet changes, and short interruptions. Two trained operators can maintain a steadier rhythm than one worker. My early estimates were too optimistic because I ignored these pauses. That mistake can affect labor planning and delivery schedules. A simple field calculation is useful: cycles per hour, blocks per mold, working hours, and an efficiency factor between 60% and 80%.
Mold capacity also affects product flexibility. A single-cavity mold may suit specialized orders, while a four- or six-cavity mold can increase output for standard blocks. However, larger capacity may require more material, stronger pallets, and careful alignment. Changing molds can take 20 minutes or longer when tools are basic. Buyers should inspect mold thickness, vibration control, spare-part access, and operator safety during a live trial. A reliable machine is one that keeps its cycle time stable after repeated production, not merely one that looks impressive during a demonstration.
What Is the Top Manual Block Machine for Global Buyers? - Comparing Cycle Time, Daily Output, and Mold Capacity Across Machines
| Machine Type |
Typical Cycle Time
(seconds) |
Mold Capacity
(blocks/cycle) |
Estimated Daily Output
(standard blocks) |
Typical Block Size
(mm) |
Approximate Footprint
(m × m) |
Best-Suited Buyer |
| Compact Manual Press |
35–45 |
1–2 |
680–1,650 |
400 × 200 × 200 |
1.2 × 0.8 |
Small contractors, startups, and low-volume projects |
| Standard Two-Cavity Manual Machine |
30–40 |
2 |
1,530–2,040 |
400 × 200 × 200 |
1.5 × 1.0 |
General-purpose block production with moderate demand |
| Four-Cavity Manual Press |
28–35 |
4 |
2,940–3,670 |
400 × 200 × 200 |
1.8 × 1.2 |
Small and medium producers seeking a balance of output and labor |
| Heavy-Duty Six-Cavity Manual Press |
35–45 |
6 |
3,670–5,250 |
400 × 200 × 200 |
2.2 × 1.4 |
Commercial yards with steady labor and higher daily demand |
| Multi-Product Manual Press |
30–50 |
2–6, depending on mold |
1,220–4,080 |
200 × 100 × 60
or 400 × 200 × 200 |
1.8 × 1.2 |
Buyers producing both pavers and masonry blocks |
Calculation basis: Daily output estimates assume one 8-hour shift, 85% operating efficiency, consistent material feeding, and standard 400 × 200 × 200 mm hollow blocks unless another size is shown. Actual output varies with mix quality, operator skill, curing workflow, mold changes, product dimensions, and site conditions.
Evaluating Hydraulic Force, Power Needs, and Manual Operating Costs
What Is the Top Manual Block Machine for Global Buyers?
Evaluating Hydraulic Force, Power Needs, and Manual Operating Costs
A strong manual block machine must balance hydraulic force with realistic operator effort. Higher pressure can improve compaction, but it may also increase maintenance demands. Buyers should check the rated force, cylinder size, mold capacity, and cycle time. These details reveal more than a sales description. A dense block needs consistent pressure, not simply maximum pressure.
Power requirements deserve equal attention. Some manual systems use hand-operated hydraulic pumps, while others need electricity for mixing or auxiliary equipment. This difference affects installation, voltage compatibility, fuel planning, and working speed. In remote areas, a hand-pump design may reduce power costs. However, it can increase fatigue and labor expenses. A cheaper machine is not always cheaper to operate.
Tips: Ask for measured cycle data, hydraulic oil requirements, and spare-part availability. Calculate labor hours per batch before choosing. Include shipping weight and local technician fees. Request independent test records where possible. Specifications can look excellent on paper, yet actual output may fall below expectations. This is worth questioning. Track production for several days before making a final investment decision.
Selecting the Best Machine Through ROI, Durability, and ISO 9001 Factors
For global buyers, the top manual block machine is not always the cheapest option. A practical choice begins with measurable ROI. Estimate daily output, labor hours, curing space, mold changes, and local transport costs. A machine producing consistent blocks can reduce rejected units and wasted cement. Ask for trial records, not only catalog promises. Field evaluations often show that simple lever systems perform better when spare parts are distant. That lesson is easy to overlook.
Manual machines depend heavily on operator technique. Check frame welds, pressing plates, hinge points, and mold thickness. Durable steel matters, but maintenance access matters too. Inspect whether grease points are reachable without dismantling the machine. Request a parts list with dimensions and material specifications. If a supplier cannot explain expected wear, reliability claims deserve caution. Very practical.
ISO 9001 is not a magic guarantee. It indicates documented quality processes, not perfect block strength. Verify certificate scope, current validity, production inspection records, and corrective-action procedures. Measure sample blocks for dimensions, edge damage, and density during acceptance testing. A written checklist protects buyers across language and distance. Still, paperwork alone is insufficient. Local water, aggregate grading, and operator training can change results sharply. Leave room for mistakes. A realistic ROI model includes downtime, training, mold replacement, and delayed sales. The best machine is one your team can operate consistently, repair responsibly, and verify with evidence.